
ProductsDetails
Multi-station Continuous Stamping Die
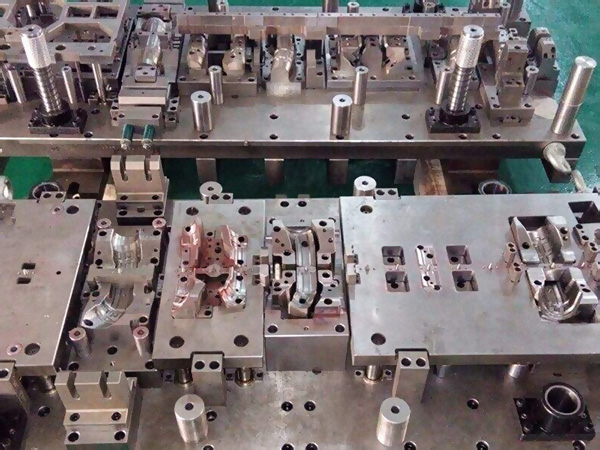
Multi-station continuous stamping die is a large, complex press tool that integrates blanking, piercing, forming, drawing, and trimming operations in a single die set. Unlike a simple progressive die that processes a narrow strip, a multi-station die handles larger and more intricate parts, carrying the workpiece through a series of operations as the press cycles.
Die Architecture
The die is built on a heavy die set with multiple guide pillars to maintain alignment under high tonnage. The lower shoe contains the die plates, while the upper shoe carries the punches and the stripper assembly. Each station is a separate insert that can be removed, repaired, or replaced independently — a major advantage for maintenance. Cam-driven side-acting stations are integrated for horizontal holes, side bends, and undercut features.
Operation Sequence
A blank is fed into the first station, where it is pierced and notched. At subsequent stations, the part is drawn, bent, embossed, and trimmed. Ejector pins lift the part after each stroke, and a mechanical or pneumatic transfer system moves it to the next station. The final station produces a finished part ready for deburring and plating.
Key Features
Handles large, complex parts that cannot be made in a single-station die.
Cam-driven side actions produce side holes, hooks, and undercuts in the same die.
Modular station inserts simplify maintenance and reduce downtime.
Nitrogen gas springs provide consistent, controllable pressure for forming pads.
Hardened working surfaces extend die life in high-volume production.
Typical Parts
Multi-station dies produce automotive structural parts, appliance panels, door hinges, seat belt components, large electrical enclosure parts, and deep-drawn housings. Material thickness typically ranges from 0.8 mm to 8 mm, and part sizes can exceed 500 mm in any dimension.
Quality Control
Each die is designed with the part's dimensional tolerance in mind. First-article parts are measured on a coordinate measuring machine (CMM) against the customer's drawing. Process parameters such as press speed, cushion pressure, and stop position are documented for repeat production runs.
Conclusion
A multi-station continuous stamping die combines multiple operations into one efficient process, reducing secondary labor and ensuring consistent part quality. It is the solution for complex, high-volume sheet metal components.
 Recommended News
-
FRP Pultruded Profiles: Material Properties and Structural Design Guide
2026-07-06 12:00:00
-
SMC and FRP Compression Molding: Design Guidelines for Parts
2026-07-06 12:00:00
-
Cooling Tower Fill Media: Material, Design and Maintenance Guide
2026-07-06 12:00:00
-
Electric Sluice Gate: Types, Actuators and Application Guide
2026-07-06 12:00:00
-
Integrated Pump Station: What It Is and How to Select the Right Model
2026-07-06 12:00:00
Contact us
—— Contact:Ms. Wang
—— Tel:+86 19948391999
—— Email:JYFRP@outlook.com
—— Url:https://www.jinyanggep.com
—— Address:Zaoqiang County, Hengshui City, Hebei Province